Rubber and plastic conveyor belts 24/7
Textile conveyor belts
WEAR-RESISTANT TEXTILE BELTS
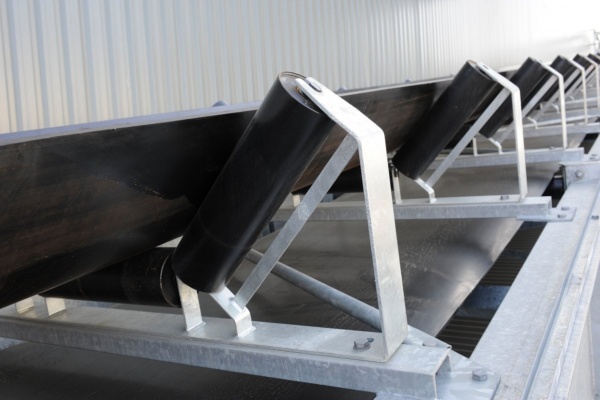
MBS supplies and installs all types of rubber conveyor belts. These wear-resistant conveyor belts are reinforced with textile and consist of polyamide and polyester fibres. That is why they are also known in the trade as textile belts.
The polyester fibres of textile belts have low elongation and are used in the warp direction. Result: optimum tension of the fabric plies. Polyamide has superior elasticity and is used in the weft direction. Result: always the correct, constant trough depth.
The carcass of these wear-resistant conveyor belts is protected by a rubber cover in cover grades (X, Y and W according to the DIN22102 standard) with superior abrasion-resistant properties.
WHICH MATERIALS?
• Sand • Coke and ash
• Cold clinker • Fertiliser
• Ores • Phosphates
• Broken glass • Wood and rushes
• Beet and chips • Raw materials
APPLICATIONS
• Quarries and mines • Port facilities
• Thermal power stations • Paper mills
• Cement works • Glassworks
• Fertiliser plants • Sugar factories
TEXTER TEXTILE BELTS
Texter textile belts of high-grade European quality were designed for even higher efficiency. These conveyor belts have a solid carcass of nylon and polyester, with reinforced cut edges and excellent adhesion between textile plies and covers.
OIL- AND GREASE-RESISTANT CONVEYOR BELTS
FULL OIL RESISTANCE (FOR)
Oil- and grease-resistant conveyor belts of FOR grade, with high resistance to conventional mineral oils and hydrocarbons. These rubber conveyor belts are available in various dimensions and weights.
MEDIUM OIL RESISTANCE (MOR)
Grease- and oil-resistant conveyor belts with or without sealed edges, resistant to vegetable or animal oils and oilseeds. MOR-grade conveyor belts are available from stock in various dimensions and weights.
APPLICATIONS
• Animal feed companies • Glassworks
• Manure processing companies • Foundries
• Automotive industry • Port facilities
• Metal recovery • Iron and steel industry
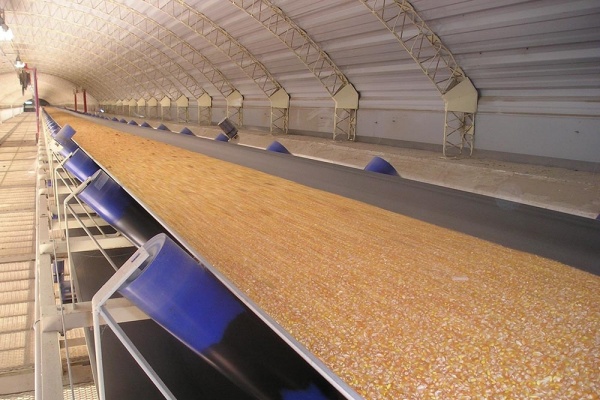
• Grain silos • Sugar factories
• Waste sorting • …
HEAT-RESISTANT CONVEYOR BELTS
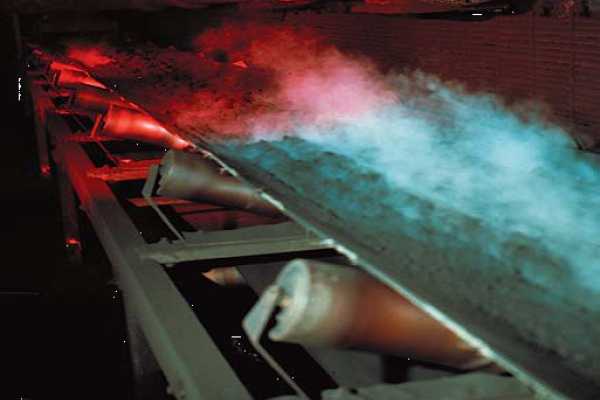
Our heat-resistant conveyor belts can cope with the most extreme temperatures. These heatproof conveyor belts were specially designed for transporting materials and raw materials at a temperature of 100 to 220 C°, depending on the specific product.
APPLICATIONS
• Chemical industry • Mining industry
• Glassworks • Salt works
• Cement works • Public works
• Blast furnaces • Iron and steel industry
FLAME-RETARDANT CONVEYOR BELTS
These antistatic and flame-retardant conveyor belts were designed to prevent accidental fires and their spread. The risk of explosions caused by static electricity is also eliminated. These fireproof conveyor belts have been extensively tested and meet the strictest safety standards. Available in classification K or S.
 Slijtvast (DIN 22102 kwaliteit Y, D of W)